To provide high-quality Pump for global customers.
Maximizing Efficiency: The Role of Rotary Lobe Pumps in Handling High-Viscosity Liquids
Nov 18,2026
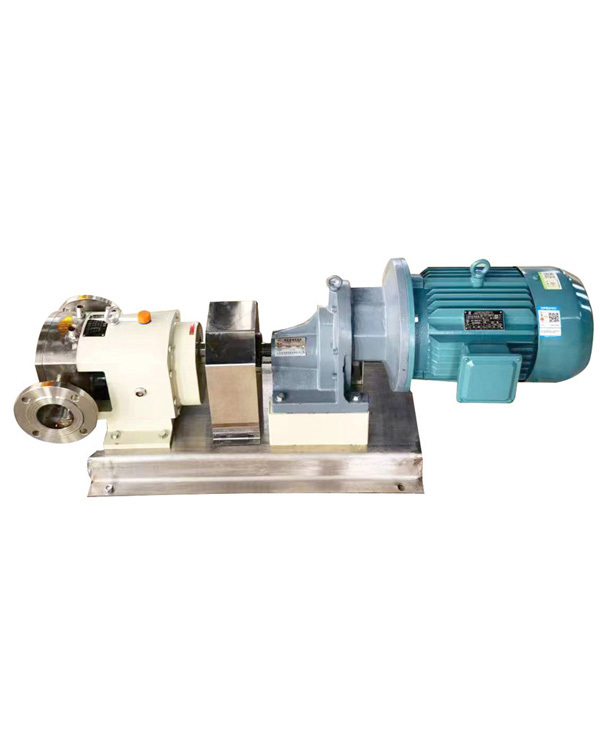
Rotary lobe pumps are increasingly recognized as a vital solution for the efficient handling of high-viscosity liquids across various industrial applications. Their unique design allows them to manage thick fluids that traditional pumps might struggle with, making them indispensable in sectors such as food processing, pharmaceuticals, and chemical manufacturing.
The operation of a rotary lobe pump involves two or more lobes that rotate within a pump chamber. As the lobes turn, they create a series of pockets that trap the fluid and move it through the pump. This design minimizes shear stress, which is crucial when dealing with sensitive materials that could be damaged or altered by excessive agitation. The ability to handle high-viscosity liquids without breaking down the product is one of the primary reasons many industries favor rotary lobe pumps.
One of the significant advantages of rotary lobe pumps is their versatility. They can handle not only high-viscosity liquids but also a wide range of other materials, including slurries, pastes, and shear-sensitive liquids. Additionally, their capacity for self-priming allows for quick and efficient operation, which is essential in processes that require minimal downtime.
Another noteworthy feature is the ease of maintenance associated with rotary lobe pumps. Many designs allow for quick disassembly and reassembly, enabling operators to perform routine maintenance or repairs without extensive downtime. This feature is particularly beneficial in industrial settings where time is of the essence. Furthermore, these pumps can be designed with various materials and elastomers to accommodate the specific chemical properties of the liquids being handled, further enhancing their adaptability.
For industries dealing with high-viscosity liquids, the selection of a rotary lobe pump should consider factors such as flow rate, pressure requirements, and the specific characteristics of the liquid being pumped. Additionally, understanding the operating environment, including temperature and potential exposure to chemicals, is crucial for selecting the appropriate materials for the pump components.
In summary, rotary lobe pumps present a powerful solution for transporting high-viscosity liquids. Their unique design promotes efficiency, minimizes shear stress, and simplifies maintenance, making them a preferred choice in various industrial applications. By understanding the operational benefits and considerations involved in choosing these pumps, professionals can make informed decisions that enhance productivity and ensure the integrity of their materials.
The operation of a rotary lobe pump involves two or more lobes that rotate within a pump chamber. As the lobes turn, they create a series of pockets that trap the fluid and move it through the pump. This design minimizes shear stress, which is crucial when dealing with sensitive materials that could be damaged or altered by excessive agitation. The ability to handle high-viscosity liquids without breaking down the product is one of the primary reasons many industries favor rotary lobe pumps.
One of the significant advantages of rotary lobe pumps is their versatility. They can handle not only high-viscosity liquids but also a wide range of other materials, including slurries, pastes, and shear-sensitive liquids. Additionally, their capacity for self-priming allows for quick and efficient operation, which is essential in processes that require minimal downtime.
Another noteworthy feature is the ease of maintenance associated with rotary lobe pumps. Many designs allow for quick disassembly and reassembly, enabling operators to perform routine maintenance or repairs without extensive downtime. This feature is particularly beneficial in industrial settings where time is of the essence. Furthermore, these pumps can be designed with various materials and elastomers to accommodate the specific chemical properties of the liquids being handled, further enhancing their adaptability.
For industries dealing with high-viscosity liquids, the selection of a rotary lobe pump should consider factors such as flow rate, pressure requirements, and the specific characteristics of the liquid being pumped. Additionally, understanding the operating environment, including temperature and potential exposure to chemicals, is crucial for selecting the appropriate materials for the pump components.
In summary, rotary lobe pumps present a powerful solution for transporting high-viscosity liquids. Their unique design promotes efficiency, minimizes shear stress, and simplifies maintenance, making them a preferred choice in various industrial applications. By understanding the operational benefits and considerations involved in choosing these pumps, professionals can make informed decisions that enhance productivity and ensure the integrity of their materials.
PREVIOUS:

Contact Us
E-mail :
sales@yaquanpump.com
service@yaquanpump.com
Phone/WhatsApp:
+44 7301702546
+63 9452052801
Address:
Room B208, Building 2, North Hongqiao Songri Center, No.215 Gaochao Road, Jiading District, Shanghai
Whatsapp: +63 9452052801
Email: service@yaquanpump.com
Room B208, Building 2, North Hongqiao Songri Center, No.215 Gaochao Road, Jiading District, Shanghai


REQUEST QUOTE